Choosing a screw compressor is not just a matter of buying the largest unit your budget allows. The right machine should match your actual air demand, operating pressure, and daily production schedule. A workshop running one shift has different needs from a plant operating around the clock. Even small details, such as pressure drops across a long pipe run or frequent start-ups, can affect performance and energy use.
Start with measured demand, not a rough guess. Review flow requirements during peak production, and consider whether future expansion is likely. Then compare fixed-speed and variable-speed models, checking efficiency across the loads your business actually uses. Air quality matters, too. If your process needs clean, dry air, include filtration and drying equipment in the system plan. Room temperature, ventilation, service access, and noise limits deserve attention before installation. They are easy to overlook.
A lower purchase price can be appealing. It may not mean lower operating costs. Ask suppliers for documented performance data at your required pressure, plus maintenance intervals and parts availability. Confirm that the proposed unit can handle your duty cycle without relying on optimistic assumptions. An experienced technician can help verify the figures against site conditions. Still, no estimate replaces sound measurements. This guide explains the main factors to assess when selecting a screw compressor, so you can compare options with clearer expectations and fewer costly surprises. Perfect sizing is rarely obvious at first. That is worth remembering.
A screw compressor should match your actual air demand, not simply the largest tool on the floor. List each air-using machine, its required pressure and flow, and how often it runs. Then note which tools operate at the same time. A small packaging line running continuously has a different demand pattern from a workshop with brief, heavy bursts. Measure it live. Record pressure and flow during busy shifts, including at the farthest point of use; pressure loss in a long or narrow pipe can make an adequately sized compressor seem undersized.
Peak demand matters, but so does the daily load profile. The U.S. Department of Energy’s Improving Compressed Air System Performance: A Sourcebook for Industry reports that leaks can waste 20–30% of compressor output in poorly maintained systems. That gap matters. Before sizing new equipment, check for leaks, pressure drops, and unnecessary air use; otherwise, the capacity calculation may simply build existing waste into the purchase. Compare measured peak flow with average demand, and account for planned production changes. A spreadsheet is useful, but it can miss short demand spikes. A temporary flow logger may reveal them. Keep the measurements, assumptions, and operating hours together so a supplier can assess the system against real conditions, rather than a single guessed number.
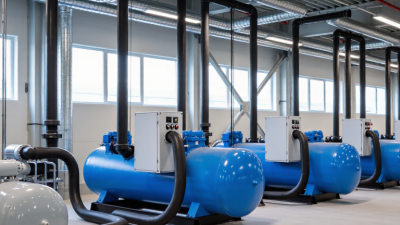
Choosing a screw compressor starts with the demand profile, not the horsepower on its nameplate. Oil-injected models suit many general plant-air applications; oil-free models reduce the risk of oil entering the process. They are not automatically the economical choice. Fixed-speed units can fit steady loads, while variable-speed models adjust output as demand changes. Real plants are less tidy: leaks and shift changes can distort the load profile.
Compare free air delivery at your required pressure, then check specific power under matching test conditions. CAGI performance datasheets help compare rated performance across models. Also review turndown range, duty cycle, cooling needs, noise, and service intervals. I still see one overlooked detail: dryer and filter pressure drops may require higher compressor pressure. The U.S. Department of Energy’s Improving Compressed Air System Performance guide reports that compressed air can use about 10% of industrial electricity, reaching 30% or more in some facilities. That makes part-load efficiency worth checking carefully. A paper rating won’t reveal every site condition.
Compare common operating-pressure ranges for oil-injected and oil-free rotary screw compressors.
The ranges shown are indicative of common industrial compressor selections, not guaranteed limits. Actual pressure capability depends on the specific model and configuration. Oil-injected compressors are often chosen for general plant air; oil-free models are designed for applications with stricter air-purity requirements. Check required flow, pressure, air-quality class, and energy use against the equipment specification.
Choose a screw compressor from measured air demand, not the largest machine that fits the room. Record flow during a full production shift, including startup peaks, pauses, and simultaneous tool use. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that compressed air uses about 10% of industrial electricity, with the share higher in some facilities. That makes poor sizing costly.
Duty cycle matters. A line running steadily needs different control from one that draws air in short bursts. Compare average demand with peak demand, then check how often the compressor will run loaded, unloaded, or stopped. DOE’s sourcebook also notes that leaks can waste 20–30% of compressor output in many plants. An air-leak survey can reveal demand that should not be used to size new equipment. This is easy to overlook.
Allow for receiver storage, pressure losses through filters and piping, and future production changes. Keep the required pressure at the point of use in view; raising system pressure to cover a restriction can increase energy use. A variable-speed unit may suit fluctuating demand, while steady demand may favor other control arrangements. Confirm both against real load data. A spreadsheet is not the whole plant; readings taken during an unusual shift can mislead. I would verify them before purchase.
| Typical Operating Pattern | Estimated Compressed-Air Demand | Indicative Compressor Size | Duty-Cycle Fit | Sizing and Control Considerations |
|---|---|---|---|---|
| Small workshop with a few air tools used intermittently | About 0.5–0.8 m³/min (18–28 cfm) while tools are running | Approximately 5.5 kW (7.5 hp); around 0.7–0.8 m³/min FAD | Low or irregular demand; a screw compressor may be suitable if use is frequent enough to justify it. | Check actual tool consumption and simultaneous use. For long idle periods, compare a smaller or alternative compressor type and consider storage capacity. |
| Regular production cell with several tools or machines | About 1.0–1.6 m³/min (35–57 cfm) | Approximately 11 kW (15 hp); around 1.3–1.6 m³/min FAD | Moderate to high demand during production shifts. | Estimate demand from equipment specifications, then account for concurrent operation and leaks. A variable-speed unit can help where demand changes substantially. |
| Busy workshop or small manufacturing line | About 2.5–3.5 m³/min (88–124 cfm) | Approximately 22 kW (30 hp); around 3.0–3.5 m³/min FAD | High, relatively steady demand over much of the shift. | Confirm the required pressure at the point of use. Check whether a single compressor can cover peak demand without excessive unloading or frequent cycling. |
| Continuous production with multiple air-consuming processes | About 4.5–6.0 m³/min (159–212 cfm) | Approximately 37 kW (50 hp); around 5.0–6.0 m³/min FAD | High duty cycle, often operating for extended periods. | Consider a lead/lag arrangement or a variable-speed trim unit if demand fluctuates. Evaluate standby requirements and the cost of production downtime. |
| Large facility with high, near-continuous demand | About 7.0–9.0 m³/min (247–318 cfm) | Approximately 55 kW (75 hp); around 7.5–9.0 m³/min FAD | Very high or near-continuous duty. | Use measured demand data where possible. Assess multiple-compressor sequencing, system pressure stability, air treatment, and future capacity needs. |
| Important: These are illustrative selection ranges, not final equipment specifications. FAD means free air delivery; actual output depends on operating pressure, inlet conditions, and compressor design. Size from measured or calculated peak demand, while also checking average demand and duty cycle. Avoid sizing from motor power alone, and include the pressure drop and air quality requirements of the complete system. | ||||
Choosing a screw compressor starts with the work your business actually does. Record operating hours, demand changes, and the pressure required at the point of use. A unit sized only for peak demand may spend much of the day running inefficiently at partial load. Ask for performance data across realistic operating conditions, not just the headline efficiency figure. Measure it first. Even a simple week of meter readings can reveal patterns that estimates miss.
Installation affects energy use, too. Long or narrow pipe runs can increase pressure losses, making the compressor work harder. Plan for adequate ventilation, safe service access, and room to remove filters or other components. Check the electrical supply and foundation requirements before delivery. These details seem ordinary. They can become expensive when overlooked. A site layout should also account for heat and condensate handling, based on the equipment specifications and local operating conditions.
Maintenance needs deserve equal attention. Ask which inspections are routine, what consumables are required, and how service intervals change with operating hours or dusty conditions. Keep records of pressure, temperature, alarms, and energy use; gradual changes may expose a problem before production is affected. A maintenance plan on paper is not enough if no one has time to follow it. Be honest about that limitation. Choose equipment and service arrangements your staff can manage consistently, and compare expected upkeep alongside purchase and energy costs.
When choosing a screw compressor, assess supplier support alongside the purchase price. A low quote can become expensive if commissioning is rushed or critical parts take days to arrive. Ask for written service response targets, local technician coverage, spare-parts availability, and a clear maintenance schedule. Request references from businesses with similar operating hours and air demand. Small details matter.
The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook estimates compressed air systems use about 10% of U.S. manufacturing electricity. Some facilities may reach 30%, according to the same report. That makes energy assumptions worth checking against measured demand, pressure, and annual operating hours. Include electricity, filters, lubricant, service visits, and downtime in your total-cost estimate. Use a realistic ownership period, such as five or ten years.
Ask the supplier to model part-load operation, not just the compressor’s rated output. Compare projected energy use with your own load profile and electricity tariff. I would question any annual-savings claim that omits those assumptions. Check warranty exclusions, maintenance intervals, and how quickly service is available during a production stoppage. A spreadsheet helps, but it cannot fully price the stress of waiting for a repair.
Please share your email with us to see your results.