Choosing the best Hole Saw For Metal starts with one simple fact: metal is not a single cutting material. Thin aluminum behaves differently from thick steel, and stainless steel can quickly expose a weak cutter. The right choice depends on the metal, its thickness, the hole diameter, and how often you will cut. There is no universal winner.
A Hole Saw For Metal should have teeth suited to the material and a shank compatible with your drill or arbor. Bi-metal models can serve general workshop tasks, while carbide-tipped designs may suit tougher metals or repeated cuts. Check the manufacturer’s stated applications rather than relying on appearance alone. Tooth count matters, but it is not the whole story. Even careful buyers can focus too much on specifications and overlook fit, stability, or cutting conditions.
Small details matter. Secure the workpiece, use a suitable cutting lubricant when recommended, and follow the saw maker’s speed guidance. Excessive heat can dull teeth and discolor the cut edge. Let the tool cut without forcing it. Keep protective eyewear on, and clear metal chips safely; they can be sharp. A pilot bit helps guide many cuts, but it must be firmly seated. Not every setup is perfect. If the saw chatters, binds, or produces heavy heat, stop and reassess the material, speed, and support. The best option is the one that cuts cleanly and safely in your actual working conditions.
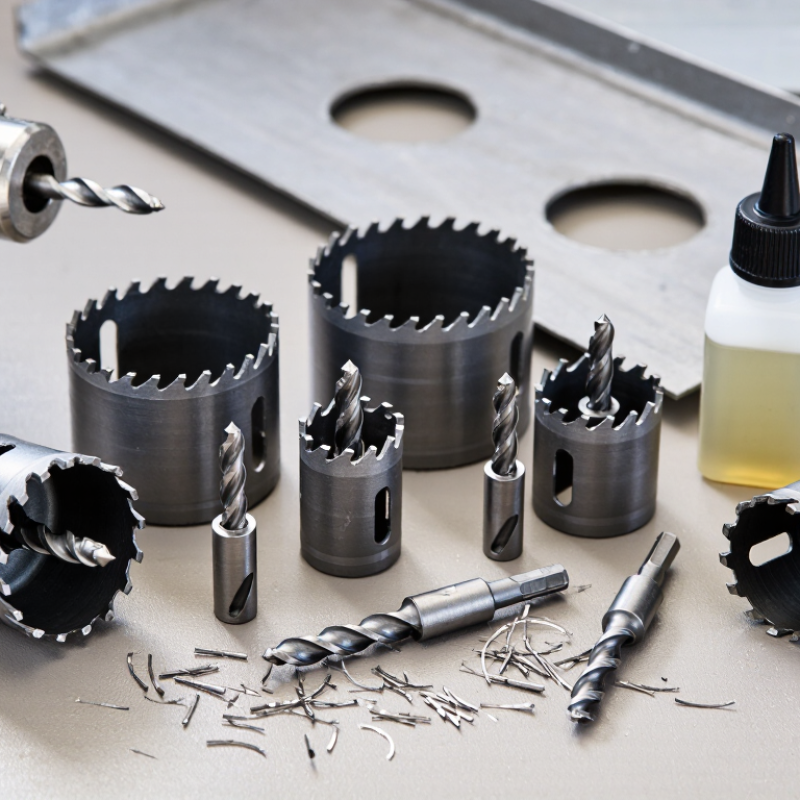
A hole saw for metal is a hollow, cylindrical cutter with teeth around its rim. Unlike a twist drill, it removes a ring of material and leaves a round metal core, called a slug. The cutter attaches to an arbor, which connects it to a drill. Many arbors include a small pilot bit. That bit helps guide the saw and reduce wandering as the teeth meet the surface.
The drill turns the saw while steady pressure brings its teeth into the metal. Cutting only around the edge takes less effort than boring a full circle, but the tool still needs careful control. Secure the workpiece, choose a cutter suited to the metal and its thickness, and follow the cutter maker’s speed guidance. Too much speed can overheat the teeth; too much pressure can bind the saw. Use suitable cutting lubricant when required, and clear chips safely. The slug may be hot. Let the tool cool before handling it. A clean hole is not guaranteed, either. Thin sheet can flex, and a pilot bit may mark the material beneath it. Checking the setup before cutting can prevent a small hole from becoming a rough one.
A hole saw’s cutting edge matters more than its appearance. For general steel, a bi-metal design pairs high-speed steel teeth with a tougher, flexible alloy-steel body. The teeth resist wear, while the body is less likely to crack under ordinary drilling stress. Look for a smooth, even weld and teeth set consistently around the rim. Small differences show up as chatter.
Tooth design affects how the saw enters and clears the cut. Variable-pitch teeth, with uneven spacing, can reduce vibration and help break up long metal chips. A modest tooth count often clears chips more freely in sheet steel; finer teeth can give a steadier cut in thinner material. For stainless steel or other abrasive metals, cobalt-alloy teeth may last longer, while carbide-tipped versions can suit demanding cuts but are less forgiving of side pressure. Match the saw to the metal, not just the hole diameter.
Keep it cool. Cutting oil and a slower, steady feed help limit heat, which can soften teeth and discolor the workpiece. Clamp thin sheet securely and let the saw do the cutting; forcing it can snag the rim. There is no perfect tooth pattern for every job. Even a good saw may cut poorly if chips pack inside the cup.
What Is the Best Hole Saw for Metal?
How to Match a Hole Saw to the Metal and Hole Size
The best choice depends on the metal, its thickness, and the hole diameter. For mild steel and occasional cuts, a bi-metal hole saw is often a practical option. Stainless steel creates more heat and resists cutting, so use a saw rated for it and work at a slower speed. Check the saw’s cutting depth against the material thickness. A shallow cup may not pass through in one cut. Small holes behave differently. Larger diameters need steady control and can bind if chips pack inside the teeth.
Tips: Clamp the work securely, mark the center, and use the pilot bit to guide the cut. Apply cutting fluid where suitable, use light pressure, and pause to clear metal chips. Wear eye protection. Let the teeth cut; forcing the saw can overheat it or snag the workpiece.
Match the saw diameter to the finished hole, not just the pilot opening. Measure twice, especially when a fitting needs a close clearance. For thin sheet metal, support the back to reduce distortion, and keep the saw square to the surface. In thicker stock, withdraw the saw periodically to clear chips and cool the cut. It may feel slower than pushing harder, but heat can dull teeth quickly. One detail is easy to overlook: hole saws leave sharp edges, so plan to deburr the opening before fitting or handling the part.
Match the hole saw’s diameter to the hole you need, then choose its cutting material for the metal and thickness.
Choosing the saw: Bi-metal hole saws are a common choice for mild steel and thinner metal. For stainless steel or tougher, thicker metal, choose a suitable carbide-tipped hole saw and follow its manufacturer’s cutting guidance. The chart shows common nominal diameters; check the product specifications before cutting.
The best metal hole saw is defined by tooth material, geometry, and heat control—not its advertised diameter alone. Bi-metal cutters combine hard high-speed-steel teeth with a tougher backing, while cobalt-alloyed teeth better retain hardness under heat. ASTM A600 specifies high-speed tool-steel grades, but it does not rank hole saws; tooth design and cutting conditions still matter. For stainless steel, look for fine, evenly spaced teeth and a rigid arbor. Variable pitch can reduce chatter. It is not a substitute for steady feed.
Cobalt content is a useful clue, not a guarantee. The USGS Mineral Commodity Summaries 2024 estimated global cobalt mine production at 230,000 metric tons in 2023; that supply figure offers context for the alloy, not proof of cutter life. For thin sheet, a finer tooth pattern helps limit snagging. For thick plate, check the saw’s cutting depth and chip clearance. Carbide-tipped teeth can cut hard materials, but they are less forgiving of vibration. Clamp the work, use suitable cutting fluid, and clear chips before they pack around the teeth. Small detail. A saw can still run hot if feed pressure is uneven, and selecting one by material label alone is an easy mistake.
A metal-cutting hole saw works safely only when its teeth match the material and its speed matches the saw’s diameter. Check the manufacturer’s speed chart; larger cutters generally need slower speeds. Clamp the workpiece firmly, and support thin sheet metal with a backing board to reduce grabbing. Wear safety glasses with side shields and hearing protection. Metal chips travel fast. OSHA’s Eye and Face Protection eTool estimates that about 2,000 U.S. workers receive medical treatment for job-related eye injuries each day. That figure covers many kinds of work, but it underscores why chip protection matters. Keep hands clear, start the pilot bit steadily, and use cutting fluid only when the saw’s instructions allow it.
Stop the drill before clearing chips or adjusting the arbor. Unplug it first. Let the teeth cool before handling the cutter; hot edges can burn skin. After each job, inspect the teeth for missing or rounded tips, check the pilot bit and arbor for looseness, then brush away chips and dry the saw. Store it where the teeth cannot strike other tools. A setup can look secure and still shift, so check the clamp again before cutting. I would not rush this check, even on a small hole. Dull teeth can wander, overheat, and make the drill harder to control; replace a damaged cutter rather than forcing it through the metal.
| Selection or safety factor | Recommended choice or practice | Practical details |
|---|---|---|
| Best all-purpose option | Bi-metal hole saw with high-speed-steel teeth | A versatile choice for many general-purpose cuts in mild steel and other common metals. Check the saw’s specifications for the material and thickness before use. |
| Harder or thicker metal | Use a hole saw specifically rated for the metal being cut; carbide-tipped designs may be suitable for some demanding applications | Tool suitability depends on the metal, its thickness, and the saw design. Follow the manufacturer’s material and thickness limits rather than relying on tooth material alone. |
| Stainless steel | Choose a saw explicitly suitable for stainless steel | Use an appropriate cutting lubricant and steady, controlled feed. Excessive heat can shorten cutting life and affect the workpiece. |
| Hole diameter | Match the saw’s stated cutting diameter to the required finished hole | Check the diameter printed on the saw or packaging, and allow for the pilot drill and arbor requirements. Available sizes vary by product. |
| Speed | Use the speed recommended for the specific saw, material, and diameter | Metal cutting generally calls for lower speeds than wood cutting. Larger diameters usually require lower speeds; do not exceed the tool or saw’s rated limits. |
| Workpiece setup | Clamp the workpiece securely to a stable surface | Do not hold small metal pieces by hand. Support the material close to the cut while keeping clamps clear of the saw’s path. |
| Personal protection | Wear safety glasses or a face shield and hearing protection | Tie back long hair and remove jewelry. Keep hands, loose clothing, and gloves away from rotating parts; follow the drill manufacturer’s safety instructions. |
| Starting the cut | Use a suitable arbor and pilot drill, and keep the saw square to the work | Start carefully so the pilot drill can guide the saw. Avoid forcing the tool or allowing the saw to tilt, which can cause binding or damage. |
| Cutting lubricant | Apply a metal-cutting lubricant when recommended for the material and saw | Lubrication can reduce friction and heat. Use it according to its label, and keep liquids away from electrical components unless the tool is designed for that use. |
| Chip removal | Stop the tool before clearing chips or removing the cut-out slug | Metal chips can be sharp and hot. Use a brush or suitable tool, not fingers, and wait for the saw to stop completely. |
| After-use inspection | Check the teeth, body, pilot drill, and arbor for wear or damage | Do not use a cracked, distorted, or badly worn saw. Replace damaged parts with components specified for the arbor system. |
| Cleaning and storage | Remove chips, dry the saw, and store it in a clean, dry place | Apply a light rust-preventive treatment when appropriate. Keep cutting edges protected and avoid storing the saw where teeth can strike hard surfaces. |
Please share your email with us to see your results.